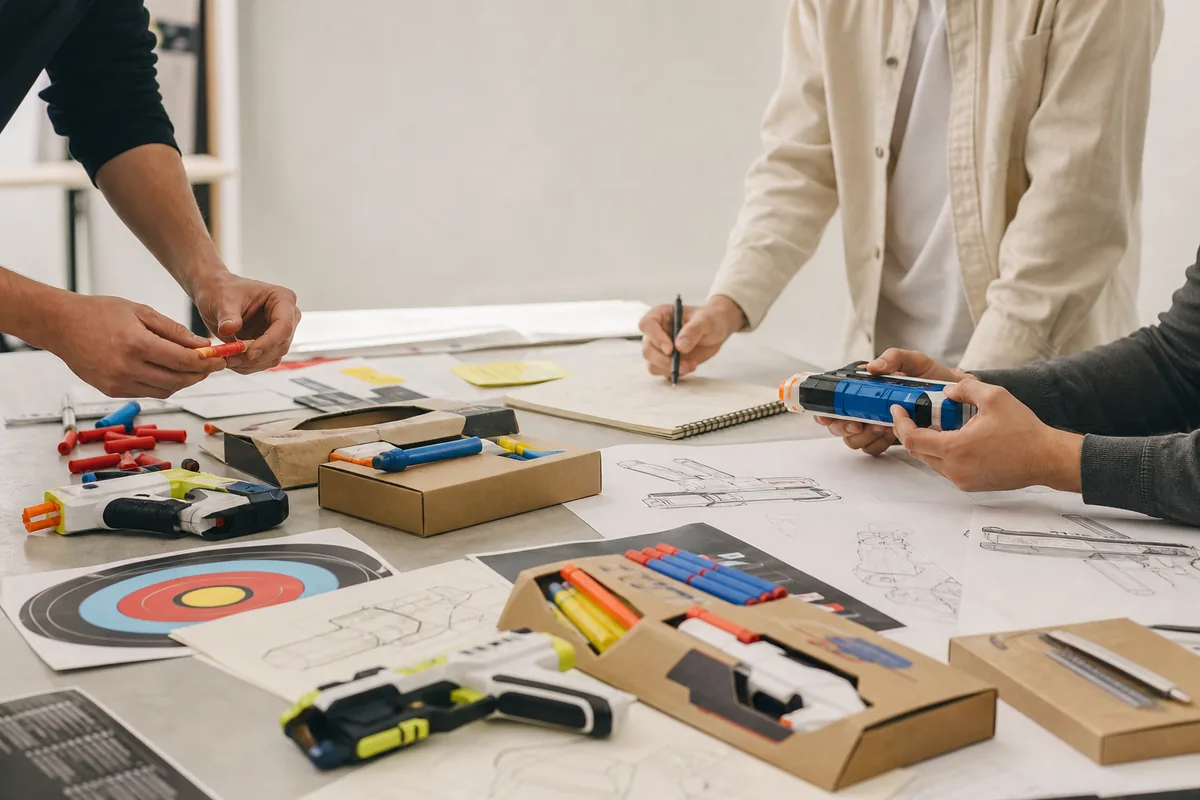
A signed golden sample is not a permanent specification, and treating it as one is the most expensive mistake repeat-order buyers make. A sealed golden sample with approved material, color, decoration, dimensions and photos is a practical production-QC reference, but it does not replace required market testing, and nothing in the available evidence shows it freezes a supplier's process across runs. The defensible position for a repeat Chenghai order is therefore narrower than most buyers assume: log deviations at defined checkpoints (golden sample, in-process inspection, carton measurement, color variables) and tie each entry to a SKU, report, responsible party and version. What you cannot do from this evidence set is claim that any specific factory, SKU or order has drifted.
Key Takeaways
- A golden sample locks appearance and dimensions as a QC reference only; it does not substitute for the market testing your destination requires, and it does not by itself hold a process in place.
- Log color against four named variables — resin grade, surface finish, lighting condition and the approved master sample — because a single approved first piece does not prove full-run consistency across cavities, shifts and material lots.
- Catch drift in dimensions, color, weight, flash, short shots and assembly during in-process checks, before the lot is complete; after packing, your options are rework, concession or scrap.
- Re-derive carton CBM from measured outer-carton dimensions every time carton size or pack quantity changes; carrying forward an old figure is how a packaging revision turns into a freight surprise.
- Treat compliance paperwork as version-bound: a test report should identify the product configuration, age grade and standard edition, so a revision that is not reflected in the report is a documentation risk, not just a spec note.
What does the evidence actually show about repeat-order drift?
The observable, recordable material in this evidence set is narrow. Four approved facts describe checkpoints where a difference can be seen and written down, plus the compliance sources that describe how documentation must be matched to a product. None of them records an actual drift event on a Chenghai order.
Checkpoint one is the golden sample itself: a sealed reference holding approved material, color, decoration, dimensions and photos. It is a production-QC tool. The same body of evidence is explicit that it does not replace required market testing — so a golden sample that matches is evidence of consistency with your approval, not evidence of compliance.
Checkpoint two is in-process inspection. Dimensions, color, weight, flash, short shots and assembly are all named as things in-process checks catch before the entire lot is complete. That list matters because these are the fields a buyer can put in a log with a value and a date, rather than a general impression that the second run "felt different."
Checkpoint three is color, and it comes with a structure. Color appearance changes with resin grade, surface finish, lighting condition and the approved master sample. If a supplier swaps resin grade or changes surface finish, an inspector comparing under different lighting can reach the opposite conclusion on the same part. Any color entry in a deviation log should therefore name which of the four changed, or state that they were held constant.
Checkpoint four is packaging and logistics. Carton CBM is derived from measured outer-carton dimensions and should be recalculated when carton size or pack quantity changes. A packaging revision — new insert, different pack quantity, a switched carton — is a measurable event, not a matter of opinion.
The compliance sources add a fifth discipline rather than a fifth checkpoint: test reports, certificates and declarations are product-, SKU-, age-grade- and version-specific, and packaging wording and product markings are controlled fields that can change with the SKU. A standard or framework is never proof that a particular factory or SKU is certified.
What can and cannot be inferred from these checkpoints?
What can be inferred is procedural. Because these checkpoints exist and are measurable, a buyer can build a repeat-order deviation log that records small differences while they are still small. That is consistent with the core claim that repeat-order drift is easiest to prevent when small differences are recorded before they become accepted practice.
What cannot be inferred is anything about prevalence, cause or supplier behavior. This evidence set contains no site catalog SKU list and no golden-sample check records, so no statement about observed drift on any actual order is supportable. There is no basis here for saying that Chenghai suppliers drift more or less than others, that a particular substitution pattern is common, or that drilling run one predicts run three.
Correlation is not causation. A color difference on run three and a supplier's resin purchase in the same month are two facts, not a cause and an effect. The four color variables tell you where to look; they do not tell you why a specific batch changed.
The gaps are specific and should be named rather than smoothed over. The approved material does not cover spring or motor substitutions, changes to dart dimensions, accessory changes, supplier notices or inspection findings — all of which appear in the briefing for this topic but not in the approved facts. Plush-material and tariff material in the wider source set is background context only and cannot be used to describe Chenghai production runs.
One more boundary matters commercially: a golden sample matching your approval says nothing about whether the product still falls inside the scope of the testing your importer relies on. Those are separate questions with separate evidence.
What should an OEM buyer do differently on the next repeat order?
Build the log before you need it. One row per repeat order, keyed to SKU and a version number, with columns for color (naming the four variables), dimensions, weight, flash, short shots, assembly, carton outer dimensions, pack quantity and derived CBM, plus any packaging or marking change. A log with those fields turns "this run looks off" into a dated entry that a supplier can answer.
Seal and distribute the reference properly. The evidence supports a sealed golden sample with approved material, color, decoration, dimensions and photos as the working reference; keep it where the inspector can reach it, and keep photographs attached to the same version number as the log. If the reference cannot be produced on request, the checkpoint does not exist in practice.
Put color in writing as variables, not adjectives. Specify resin grade, surface finish and the lighting condition under which color is judged, and name the approved master sample. A PO that says "same as last time" invites exactly the ambiguity the four variables exist to remove.
Re-check packaging numbers whenever anything about the pack changes. Carton dimensions and pack quantity feed CBM; a new insert or a different pack count means the CBM is re-derived, not inherited. This is cheap to verify at the factory and expensive to discover at the port.
Keep compliance paperwork aligned to the version you are actually shipping. Because a test report should identify the product configuration, age grade and standard edition, and because packaging wording and markings are controlled fields, route any color, dimension, packaging or accessory change past the person who holds the report — before the PO, not after the shipment.
Where the evidence runs out, mark it unknown. This evidence set does not support claims about spring or motor substitution behavior, dart dimensions, accessory-change frequency, supplier notices or inspection findings on Chenghai orders, and it does not support any MOQ, price, lead-time or certification-status statement for a specific factory. If those points decide your order, get them from your own check records and your supplier's written notice, and record the answer.
Evidence and limits
| Claim: A sealed golden sample with approved material, color, decoration, dimensions and photos is a practical production-QC reference; it does not replace required market testing. | Source: approved fact (golden sample lock). Limitation: establishes a QC reference only; no statement about any factory, SKU or order, and no evidence that a matching sample equals compliance. |
|---|---|
| Claim: In-process checks catch drift in dimensions, color, weight, flash, short shots and assembly before the lot is complete. | Source: approved fact (in-process checks). Limitation: identifies detectable fields, not observed frequencies; no evidence supplied that any of these drifted on a Chenghai order. |
| Claim: Color appearance depends on resin grade, surface finish, lighting condition and the approved master sample. | Source: approved fact (color matching). Limitation: names the variables to control; it does not explain why a specific batch changed, and a single approved first piece does not prove full-run consistency across cavities, shifts and material lots. |
| Claim: Carton CBM is derived from measured outer-carton dimensions and should be recalculated when carton size or pack quantity changes. | Source: approved fact (packaging CBM). Limitation: a measurement rule only; no freight, duty or landed-cost figure is supported by this evidence set. |
| Claim: A drawing or 3D-model revision should be linked to the tooling, FAI, test sample and production order so an old file cannot silently return to use. | Source: approved fact (drawing revision control). Limitation: describes document control, not tooling condition, shot life or any specific factory's practice. |
| Claim: Toy products placed on the EU market must meet the applicable essential safety requirements; CE marking and an EU Declaration of Conformity belong to the conformity process and must be matched to the product scope. | Source: Toy Safety Directive 2009/48/EC. Limitation: framework-level statement; check the current consolidated text, market and product scope, and never read it as certification of a specific factory or SKU. |
| Claim: Children's toys generally require testing at a CPSC-accepted laboratory and a Children's Product Certificate, which is based on testing results and identifies the applicable rules and responsible parties. | Source: CPSC toy safety business guidance and Children's Product Certificate page. Limitation: a CPC is product-specific and should not be described as a blanket factory certificate; the product, age grading and applicable rule set must be mapped before any compliance statement. |
| Claim: A test report should identify the product configuration, age grade and standard edition, and the applicable edition should be read from the current regulation before a report is quoted. | Source: 16 CFR Part 1250 / ASTM F963 and the ASTM F963 standard page. Limitation: no report, certificate number or test result for any Chenghai product is supplied here; edition and incorporated status must be checked before quoting. |
| Claim: Tracking information should be permanent and support product identification where applicable; packaging, product markings and lot control should be reviewed together. | Source: CPSC tracking labels guidance. Limitation: supports a review discipline for markings and lot control; it does not establish what any specific supplier prints. |
| Claim: Age grading and small-part risk are connected and must be assessed for the actual product configuration, including assemblies, detachable accessories and packaging components. | Source: CPSC small parts guidance. Limitation: requires review of the actual configuration; no statement about a specific product's age grading or small-part status. |
| Claim: Repeat-order drift observations on Chenghai orders, including spring or motor substitutions, dart dimensions, accessory changes, supplier notices and inspection findings. | Source: none supplied. Limitation: unknown. The required site catalog SKU and golden-sample check records were not provided, so no observation about actual repeat-order drift can be made from this material. |
FAQ
Does the evidence prove that Chenghai suppliers drift on repeat orders?
No. The supplied material contains no site catalog SKU list and no golden-sample check records, so it supports a checkpoint-and-record method but no statement about observed drift on any actual order. Treat any specific drift claim as something you must establish from your own inspection records.
My color looks different on run three. What should I actually check first?
Check the four variables that change color appearance: resin grade, surface finish, lighting condition and the approved master sample. Because a single approved first piece does not prove full-run consistency across cavities, shifts and material lots, compare parts from more than one cavity and shift, and record which variable changed rather than describing the color as "off."
How early can a deviation be caught, and what does that mean for cost?
In-process checks catch drift in dimensions, color, weight, flash, short shots and assembly before the entire lot is complete, which is the last point where rework is cheap. Ocean transit runs well beyond that window, so a deviation found at pre-shipment inspection usually means a concession, a rework scramble or a split shipment rather than a clean fix.
If I change the packaging or the pack quantity, what should I re-verify?
Recalculate carton CBM from the measured outer-carton dimensions, because CBM is derived from those measurements and should be re-derived whenever carton size or pack quantity changes. Packaging wording and product markings are also controlled fields tied to the SKU, so route the change past whoever holds your test report before the PO is issued.
Does a matching golden sample mean my compliance documents are still valid?
No. A golden sample is a production-QC reference and does not replace required market testing. Test reports and certificates are product-, SKU-, age-grade- and version-specific, and a test report should identify the product configuration, age grade and standard edition — so a color, dimension, packaging or accessory change needs to be checked against the document, not assumed covered.
Can I rely on this material for MOQ, pricing or certification status of a specific factory?
No. This evidence set supports no MOQ, price, lead-time or certification-status statement for any specific factory, and a standard or framework is never proof that a particular factory or SKU is certified. Get those answers in writing from the supplier and record them against the SKU and version.
Sources
Request a Quote
If you are setting up a repeat-order deviation log for foam blaster and target-set programs, we can walk through the checkpoint fields with you — color variables, in-process findings, carton measurement and version control — and quote against your actual specification. Start with the 3-Mode DIY Motorized Foam Dart Blaster (https://www.FoamBlasterSource.com/products/3-mode-diy-motorized-foam-dart-wholesale/) or the Motorized Foam Dart Rifle Blaster (https://www.FoamBlasterSource.com/products/motorized-foam-dart-rifle-bla-sb524b-wholesale/), and tell us which fields you want recorded per run.